Grown structure.
Composite components and functional coatings, grown rather than laid up. Hemp bench validated. Zoned parts in build.
Hemp composites tested, zoned parts in build.
The part arrives in pieces.
Composite parts ship from overseas. Long lead times, freight cost, prices outside of your control.
A shielded enclosure, an antenna window and a load path are three separate parts joined at bonded seams. Every seam is a step, an inspection, and a place the assembly can fail.
Designed for purpose. Grown by zone.
Inoculate the mould and the colony binds across the whole form. Anything placed in it beforehand — conductive mesh, fibre reinforcement, mounting hardware — is incorporated as the part grows.
Put the avionics bay inside an RF mesh enclosure. Put the antenna in a second cavity with none. Conventional layup needs three parts and two bonded seams. Ours comes out of one mould.
Density is a variable, not an outcome. Internal geometry is free.
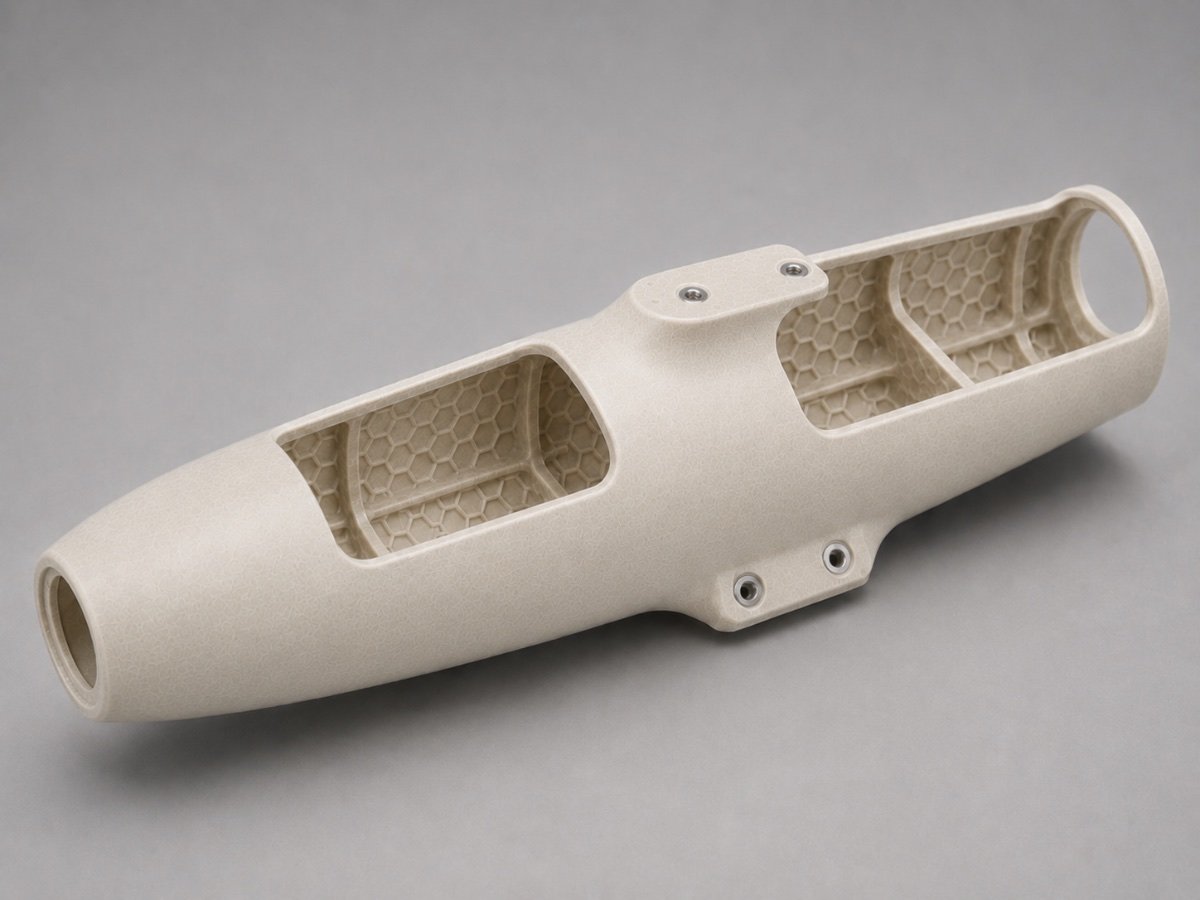
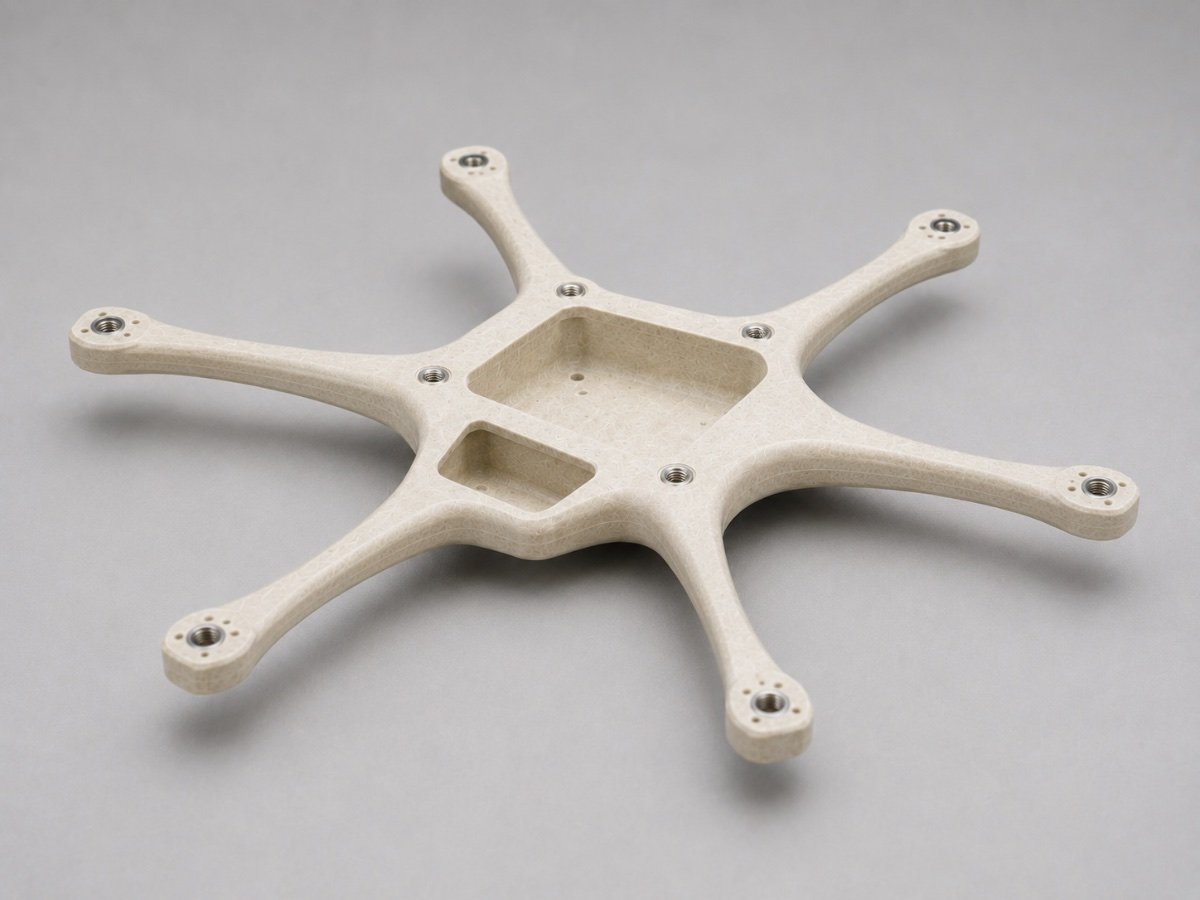
Hemp, straw, sawdust, corn husk. Whatever the region already throws away.
How we prepare it matters more than what it is. We source locally and control the outcome in the process.
| Density | Low, controllable through thickness |
|---|---|
| Dielectric | Low-loss — antennas integrate conformally, no cut-in window |
| Thermal conductivity | Low |
| Reinforcement | Woven skins and selective fibre, placed pre-growth |
| Shielding | Conductive mesh, zoned |
Our own mesh network runs on exactly this property.
Figures for our formulation will be published as they are measured.
| Flame | Chars rather than drips |
|---|---|
| Edges | Cut edges sealed in place |
| Moisture | Barrier layer, controlled thickness |
| Encapsulation | Inserts and hardware sealed at the interface |
| Repair | Brush or spray, in the field |
| End of life | Degrades on a chemical trigger |
The cultivation process, the sterilisation method, the coating chemistry, and the process control.